Why Small Shops Are Finally Pulling the Trigger on Robotic Welding

A chronic shortage of skilled welders, demand for higher throughput, and rising wage pressure have flipped the “automation is for big shops” assumption. Small fabrication shops are adopting compact robotic welding cells to maintain production levels, scale output without requiring new hires, and meet strict contractor deadlines.

Small shops with $1 million to $25 million in revenue are now prime candidates to make the switch to a robotic welding system. According to the American Welding Society there was a 400,000-welder shortage in 2025. Robotic welding for small shops can help meet output without sacrificing margins. Cobots and compact cells as small as 15 sq. ft. make robotic welding viable in existing floor space. The real question isn’t are we big enough? The question should be: Which parts in our mix run long enough to justify a robotic cell?

This is where Capital Machine Technologies can help. Our advisory process includes evaluating current production bottlenecks, projecting capacity needs, and recommending technology-matched solutions that meet your shop’s application needs. We are a dealer, service provider, and value-added distributor that not only has the top-of-the-line robotic welding systems for sale, but we also provide comprehensive services that keep equipment working.

Contact Us Today

Cobots vs. Industrial Robots: Which One Fits Your Floor?

The practical difference between a cobot and an industrial welding robot boils down to safety, programming, and production scale. Collaborative robots, or cobots, are designed to share a workspace with humans, feature easy hand-guided teaching, and suit low-volume batches. Industrial robots require safety cages, need complex programming, and are built for high-volume mass production. Cobot welders win on ease of deployment, small footprint, and hand-guided teaching. Industrial robots win on speed and duty cycle for repeat runs.

Welding cobots make the most sense for low-volume, high-mix production, frequent station changes, or applications requiring close human collaboration. They are ideal when you lack floor space for bulky safety enclosures, need to automate quickly on a budget, or have part and tool payloads under 30 kg.

Power and Force Limiting (PFL) lets cobots work alongside operators without guarded cages, which matters when floor space is tight (ISO 10218/TS 15066) on cage-free collaborative operation.

Many shops start with a cobot for prototyping and low-volume jobs, then add an industrial cell as volume ramps. Capital Robotics, a division of Capital Machine, supports both paths with Yaskawa Motoman and OTC Daihen systems. We specialize in manufacturing modular robotic weld cells, such as our signature Fusion Arc Welding System, and supplying integrated Metal Inert Gas (MIG) welding and Tungsten Inert Gas (TIG) welding, plasma, and laser welding cutting machines.

The Readiness Checklist Before You Sign a Purchase Order

Readiness Question Checklist

  • Does your shop have parts that require consistent, repeatable welds?
  • Are monthly volumes large enough to justify the move to a robotic cell?
  • Will your fixturing need to be updated to ensure reliable automated welding?
  • Do your applications have predictable joint locations with stable fit-up conditions?

Robotic welding is typically a strong fit for parts that require consistent, repeatable welds and are produced in moderate to high volumes. Parts with predictable joint locations, stable fit-up conditions, and relatively simple weld access tend to perform best in an automated environment.

Larger weldments, multi-pass welds, and components requiring long arc-on times are good candidates as a robotic welding system can improve cycle time consistency and reduce operator fatigue. Manufacturers often see the greatest value when welding processes are repetitive and quality requirements are strict, since robotic systems can deliver more uniform weld penetration, bead appearance, and travel speed than manual welding.

Part stability and dimensional consistency are also important considerations. Automated welding relies on repeatability, so excessive variation in incoming material, cut quality, or part geometry can create programming and quality challenges.

Implementing robotic welding often requires updates to fixturing and part design to improve repeatability and ensure reliable welding automation performance. Fixtures typically need to provide more precise and consistent part location than manual welding setups as robots follow programmed paths with very little tolerance for variation.

Space, Power, and What Your Building Actually Needs

Space Needs

A small-shop robotic welding cell can often fit into roughly 200 to 600 sq. ft, but the actual footprint depends on the robot arm size, part dimensions, safety requirements, and level of automation. A basic single-robot cell with a welding table, safety fencing, and power source may only require an area around 15′ x 15′ to 20′ x 20′ for smaller parts and lower-volume production.

Electrical Power Requirements

Electrical and fume-extraction requirements for a robotic welding cell vary based on the welding process, welding applications, robot size, duty cycle, and facility layout, but most systems require planning for power capacity, ventilation, and environmental safety well before installation.

A typical robotic welding cell will need dedicated electrical service for the robotic welder, welding power source, positioners, safety systems, and peripheral equipment such as conveyors or fume collectors. Many industrial robotic welding systems operate on three-phase power, although smaller shop systems and cobot welding cells may use lower voltage configurations depending on the equipment. Shops also need to account for adequate grounding, disconnects, surge protection, and network connectivity for controls, monitoring, and programming systems.

Capital Machine offers shops installation supervision that covers the technical sequence with a pre-install site survey to verify floor specifications and utility access, machine calibration once the rigger completes physical placement, first run testing to validate quality and performance parameters, and operator sign-off confirming the machine meets acceptance criteria.

Small-Shop ROI: How the Math Actually Works

A realistic payback period for a first robotic welding cell is often between 12 and 36 months, depending on production volume, labor availability, weld complexity, and how consistently the system is utilized. Shops that struggle with welder shortages, overtime costs, rework, or throughput bottlenecks frequently see faster returns because automation can improve arc-on time, weld consistency, and production predictability.

However, many manufacturers underestimate costs related to fixturing, part standardization, operator training, maintenance support, facility preparation, and integration downtime during startup. Some shops also overlook indirect costs such as electrical upgrades, fume extraction, programming support, and future tooling changes.

Tax incentives like Section 179 expensing and bonus depreciation can significantly improve the financial picture by allowing manufacturers to deduct a large portion, or in some cases the full cost, of qualified equipment investments in the year the system is placed into service. This can reduce taxable income, improve cash flow, and shorten the effective payback timeline for companies investing in automation.

Programming a Welding Robot Without a Robotics Engineer on Staff

Many modern universal robot welding systems are designed so experienced welders without prior programming backgrounds can learn to operate them successfully. Today’s systems often use intuitive interfaces that simplify robot setup and adjustment, allowing welders to apply their welding knowledge without needing advanced coding skills.

Hand-Guided

Hand-guided teaching, commonly used with cobots, allows operators to physically guide the robot arm through weld paths while the system records movement points and parameters. One fabricator reported a new hire running a cobot weld job in 20 minutes.

Offline Programing

Offline programming (OLP), on the other hand, involves creating and testing robot programs on a computer simulation before sending them to the welding cell, which helps reduce production downtime and supports more complex automation environments.

Operator training timelines vary based on system complexity, but many welders can learn basic operation, part loading, touchups, and routine programming adjustments within a few days to a few weeks. More advanced programming, troubleshooting, fixture setup, and optimization skills typically develop over time with continued production use and hands-on experience.

Capital Machine also offers operator training at our Atlanta, Georgia training facility or on-site at your facility. Your operators will learn the system they will actually weld on, saving valuable production time.

Service, Uptime, and What Happens After the Truck Leaves

Capital Machine sets itself apart from other vendors with our post-purchase support. We are a dealer, service provider, and value-added distributor that not only has the top-of-the-line machines for sale, but we also provide comprehensive services that keep equipment working.

Our 43-factory-trained field service engineers have parts-stocked vans and are ready to diagnose and service your equipment across our 22-state territory. Our engineers are backed by a 53-member service department ready to assist you. We offer condition-based maintenance programs, operator training and retraining, and application support. We provide the largest dedicated service network in the United States, backed by more than 40 years of fabrication equipment expertise. For more information visit our service page.

Your 90-Day Path from First Conversation to First Good Part

Our process for adding a robotic welding cell includes a part-fit audit, cell selection, fixturing design, install and calibration, operator training, and first-article approval with system design and build typically 8-16 weeks and commissioning at 2-4 weeks.

Capital Machine’s advisory process includes evaluating your current production bottlenecks, projecting capacity needs, and recommending technology-matched solutions that meet your shop’s application needs. The goal is the right cell for your shop’s application mix. Contact us to learn more.

Plasma, Laser, or Waterjet: A One-Minute Verdict

If you only read one section of this guide, here’s the short answer to the plasma vs laser vs waterjet debate:

  • Choose laser cutting if your shop primarily processes thin-to-medium gauge sheet metal and you need the highest speed, precision, and edge quality.
  • Choose plasma cutting if you regularly cut thick conductive metals and the lowest cost-per-foot of cut.
  • Choose waterjet cutting if you need to cut materials that thermal processes cannot handle, or if your parts cannot tolerate a Heat-Affected Zone (HAZ).

The single biggest factor driving this decision is your material profile.

  • Is the material metal or non-metal?
  • Is it electrically conductive?
  • What thickness range do you process most often?

These answers usually narrow the field quickly.

A fabrication shop processing mostly stainless and mild steel under ½ inch thick will likely benefit most from a fiber laser. A heavy plate fabricator working with 1-inch to 3-inch steel may find a plasma cutting machine provides the best return on investment. A manufacturer cutting composites, glass, stone, rubber, or heat-sensitive alloys will often require a waterjet cutter.

Many successful shops actually run more than one technology. A common pairing is laser cutting and plasma cutting, where the laser handles precision sheet work and the plasma system handles thicker materials. Another popular combination is laser plus waterjet, allowing a shop to process both precision metal components and heat-sensitive or non-metal materials.

One advantage of working with Capital Machine is that the recommendation is not predetermined by a single product line. Capital Machine sells, installs, and supports Messer Cutting Systems plasma and oxyfuel equipment, Mazak fiber laser systems, and OMAX waterjet solutions. That means customers can evaluate all three technologies objectively and select the best fit for their production goals.

Contact Us Today

The Comparison Matrix at a Glance

When evaluating plasma vs laser vs waterjet, most buyers focus on four key factors: speed, precision, cost, and material compatibility.

Speed

Each technology dominates a different application range.

  • Laser cutting is generally the fastest option for thin metal and medium-thickness sheet metal.
  • Computer Numerical Control (CNC) plasma cutting excels on thick conductive plate.
  • Water jet cutting is typically the slowest process, especially as material thickness increases.

Precision

Precision differences can significantly affect downstream operations. A laser cutter produces extremely accurate parts with excellent edge quality. A waterjet can achieve even tighter tolerances because the process introduces virtually no thermal distortion.

  • Plasma: Approximately ±0.020 inch
  • Laser: Approximately ±0.002 inch
  • Waterjet: Approximately ±0.001 inch

Kerf Width

Kerf width affects nesting efficiency and material utilization. The narrower kerf produced by a laser cutter allows shops to maximize material yield from expensive sheet stock.

  • Laser: 0.4 mm
  • Waterjet: 0.6 mm
  • Plasma: 3.8 mm

Cost

Cost varies considerably between technologies.

  • Plasma cutting offers the lowest machine acquisition cost and low operating costs.
  • Laser cutting generally delivers favorable operating economics through speed and automation.
  • Waterjet cutting requires abrasive garnet, making consumable costs higher.

Heat-Affected Zone

HAZ is often a deciding factor. For shops concerned about metallurgical changes, distortion, or heat-sensitive materials, a water jet may be the best solution.

  • Waterjet cutting is a cold-cutting process with essentially zero HAZ.
  • Laser cutting creates a small HAZ.
  • Plasma cutting creates the largest HAZ of the three.

Ultimately, specification sheets only tell part of the story. Our five technology centers are a great place to test out your shop’s applications. Our centers are under power so you can test out our systems under real world conditions. Our technology centers are located in Tampa, Florida; Atlanta, Georgia; Dallas, Texas; Indianapolis, Indiana; and Harrisburg, Pennsylvania.

Plasma Cutting: Fast and Cost-Effective on Thick Conductive Metal

Plasma cutting works by creating an electrically conductive channel of ionized gas. This high-temperature plasma arc melts metal while a high-velocity gas stream removes molten material from the cut. As the process depends on electrical conductivity, a plasma cutter only works on conductive metals such as mild steel, stainless steel, aluminum, and copper. This limitation is also one of its strengths.

A modern plasma cutting machine delivers exceptional productivity on heavy plate applications. Industrial systems commonly process material from ½ inch to over 1.5 inches thick, while high-amperage systems can cut 2-inch to 3-inch plate effectively.

Strengths of Plasma Cutting

  • Low cost per linear foot.
  • High cutting speed on thick material.
  • Ability to process large steel plates.
  • Lower capital investment than many laser systems.

For many fabrication shops, CNC plasma cutting remains the most economical solution for thick steel production. However, plasma does have limitations. Compared with a laser cutter or waterjet cutter, plasma produces a wider kerf, larger heat-affected zones, more dross, and less precise edge quality. Secondary finishing may be required when parts demand tight tolerances or cosmetic-quality edges.

Fortunately, modern high-definition plasma technology has significantly narrowed the performance gap. Advanced systems can achieve edge quality that approaches laser performance on certain mid-thickness applications. Capital Machine distributes and supports Messer Cutting Systems, such as the MetalMaster Evolution, MPC2000, and MPC2000 MC. These platforms cover the full range of plasma cutting applications while also supporting drill units, marker heads, and oxyfuel cutting capabilities for increased versatility.

Laser Cutting: Precision and Speed on Thin-to-Mid Metal

When most manufacturers think about modern metal fabrication, they think about laser cutting. Industrial laser processing today is dominated by fiber laser systems that operate at a wavelength of approximately 1.06 micrometers, making them exceptionally effective for processing metals. Traditional CO2 lasers remain useful for non-metal applications such as wood, acrylic, leather, and plastics. However, for industrial sheet metal processing, the fiber laser has become the standard.

Laser Cutter Advantages

  • Exceptional precision
  • Narrow kerf widths
  • Outstanding edge quality
  • High processing speed
  • Strong automation potential

When cutting thin material, a fiber laser often outperforms both plasma and waterjet by a substantial margin. For manufacturers producing electrical enclosures, HVAC components, brackets, cabinets, and precision metal parts, laser systems frequently provide the lowest cost per part. Modern laser cutters can safely process reflective materials such as copper and brass, materials that once posed challenges for older laser technology.

Still, every technology has limits. While high-power systems continue pushing boundaries, laser cutting generally reaches its economic thickness ceiling between approximately 15 mm and 25 mm depending on material type and laser power. At some point, plasma cutting becomes the faster and more economical solution for thicker materials.

Capital Machine offers several Mazak laser platforms, such as the OPTIPLEX NEO, OPTIPLEX FIBER III, and OPTIPLEX Ez. These systems range from entry-level production equipment to high-output manufacturing solutions designed for demanding fabrication environments. Many growing fabrication companies adopt a two-machine strategy. A fiber laser handles the majority of daily sheet metal production while a plasma or waterjet system covers specialized work outside the laser’s sweet spot.

Waterjet Cutting: The Cold-Cutting Universal Solvent

If laser cutting and plasma cutting dominate metal production, waterjet cutting dominates versatility. Abrasive waterjet cutting uses ultra-high-pressure water, typically between 30,000 PSI and 90,000 PSI, mixed with garnet abrasive. The resulting stream erodes material rather than melting it.

This process creates a remarkable advantage. Virtually no heat enters the workpiece. As water jet cutting is a cold-cutting process, it avoids heat distortion, thermal stress, metallurgical changes and heat-affected zones. That makes waterjet cutting ideal for materials that cannot tolerate heat. A waterjet cutter can process steel, stainless steel, aluminum, titanium, copper, stone, glass, ceramics, rubber, foam, and composite materials. Few manufacturing technologies offer this level of material compatibility.

Another significant advantage is thickness capability. Depending on the application, a water jet can cut materials up to 24 inches thick for rough-cut operations. The trade-off is speed. Compared with laser cutting and plasma cutting, waterjet cutting is slower. Garnet abrasive also contributes meaningful operating expenses. Waterjet systems require infrastructure for water treatment and abrasive handling, increasing floor-space requirements. Despite these considerations, many industries rely heavily on waterjet technology.

Capital Machine distributes OMAX waterjet systems because they solve problems that thermal cutting simply cannot address. In aerospace, marine, defense, and food-processing applications, maintaining the original properties of a heat-treated component can be critical. A waterjet cutter preserves those properties while delivering precise cuts across an enormous range of materials.

Head-to-Head: Plasma vs Laser, Plasma vs Waterjet, Laser vs Waterjet

Plasma vs Laser

In the plasma vs laser comparison, the answer depends largely on thickness. Choose laser cutting when processing thin material, prioritizing precision, requiring excellent edge quality, and maximizing throughput on sheet metal. Choose plasma cutting when processing thick conductive metal, prioritizing low operating costs, and cutting heavy plate. For shops processing mostly metal under 10 mm thick, a laser cutter is often the clear winner.

Plasma vs Waterjet

The plasma vs waterjet decision centers on speed versus flexibility. Choose plasma when cutting conductive metals, prioritizing speed, and minimizing operating costs. Choose waterjet cutting when processing non-conductive materials, eliminating heat-affected zones, and cutting extremely thick material. If heat distortion is unacceptable, water jet cutting generally wins.

Laser vs Waterjet

The laser vs waterjet comparison is one of the most common buying decisions today. Choose laser when processing mostly sheet metal, prioritizing speed, and seeking lower per-part costs. Choose waterjet when cutting diverse materials, requiring zero HAZ, and processing composites, stone, or glass. Many advanced manufacturers ultimately install both technologies to maximize flexibility.

Capital Machine’s ability to provide Mazak, Messer, and OMAX equipment under one roof allows buyers to compare complete production strategies rather than isolated machine specifications. We offer a consultative approach to shops. Every engagement starts with understanding your challenges, production requirements, and facility constraints. Our advisory process includes evaluating current production bottlenecks, projecting capacity needs, and recommending technology-matched solutions that meet your shop’s application needs.

Best-Fit Recommendations by Industry and Job Profile

High-Mix Job Shops

For shops processing a broad range of sheet metal parts under 20 mm thick, a fiber laser is usually the best investment.

Heavy Plate and Oil & Gas

Heavy fabrication operations often favor plasma cutting combined with oxyfuel technology. Messer’s MetalMaster Evolution and MPC2000 platforms excel in these demanding environments.

HVAC and Electrical Enclosures

Precision, speed, and automation make laser cutting the dominant solution.

Aerospace, Defense, and Marine

These sectors frequently rely on waterjet cutting because zero HAZ is critical when processing titanium, composites, and heat-treated components.

Sign and Packaging Industries

For non-metal materials such as acrylic and wood, CO2 lasers remain highly effective and often represent a better value than a waterjet solution.

Capital Machine’s experience across automotive manufacturing in the Midwest, oil and gas production in Texas, aerospace operations in the Carolinas, and marine fabrication in Florida helps guide customers toward the most practical configuration for their region and application.

Final Recommendation and How to Validate Before You Sign

The best way to settle the plasma vs laser vs waterjet debate is to test your actual parts. Bring your most challenging 5 to 10 production components to a Capital Machine technology center and run them on all three technologies. Real-world cutting data is far more valuable than theoretical specifications.

Before purchasing, request a written cost-per-foot model that reflects your materials, your production volume, your labor assumptions, and your throughput requirements. You should also evaluate service response times, parts availability, training programs, installation support, and long-term application assistance.

Capital Machine sets itself apart from other vendors with our post-purchase support. We are a dealer, service provider, and value-added distributor that not only has the top-of-the-line machines for sale, but we also provide comprehensive services that keep equipment working.

Our installation supervision covers the technical sequence with a pre-install site survey to verify floor specifications and utility access, machine calibration once the rigger completes physical placement, first run testing to validate cut quality and performance parameters, and operator sign-off confirming the machine meets acceptance criteria.

Our 43-factory-trained field service and preventive maintenance engineers have parts-stocked vans and are ready to diagnose and service your equipment across our 22-state territory. Our engineers are backed by a 53-member service department ready to assist you. We offer condition-based maintenance programs, operator training and retraining, and application support. We provide the largest dedicated service network in the United States, backed by more than 40 years of fabrication equipment expertise.

Why Laser Cutter Selection Is Really a Power-Selection Decision

When manufacturers begin evaluating a new laser cutter, they often focus first on table size, automation options, software features, or even brand preference. In reality, the most important decision in any industrial laser cutter selection process is much simpler: choosing the correct power level. For modern fiber laser cutting machine applications, power rating is the specification that drives nearly every other aspect of performance. The kilowatt (kW) rating determines the maximum material thickness you can process, how quickly you can complete parts, and overall operating economics of the machine. While bed size, controls, and automation certainly matter, none of them can compensate for selecting the wrong power tier.

An underpowered fiber laser cutter may force a shop to decline thick-plate opportunities, slow production schedules, and operate at the speed of its most demanding cuts. Conversely, an oversized laser machine can burden a company with unnecessary capital expense, increased power consumption, and operating costs that never translate into additional revenue. Power also has a direct effect on return on investment. Faster cutting speeds reduce cycle times, increase throughput, and improve machine utilization. In many cases, the right power tier can have a greater financial impact than any software upgrade or automation package.

This is why experienced machinery advisors, like Capital Machine, begin every conversation with power requirements. At Capital Machine, power is typically the first discussion point when evaluating a customer’s application needs. Once the appropriate power level is established, factors such as bed size, automation, software, and material handling can be layered into the recommendation.

Power Tiers Decoded: 6 kW, 10 kW, 15 kW, and 20 kW 30kw

Understanding industrial laser power tiers is critical when evaluating a Computer Numerical Control (CNC) laser cutting machine.

2kW-3kW

The 2kW–3kW category is ideal for shops focused primarily on thin-gauge sheet metal. These systems
handle mild steel under approximately 6mm efficiently and often represent a logical upgrade path from older CO2 laser technology. Many job shops entering the world of fiber laser processing start here as the initial investment is lower while still delivering significant productivity gains over traditional fabrication methods.

4kW–6kW: The Workhorse Range

For most fabrication businesses, 4kW–6 kW is the sweet spot. This power range supports the majority of general sheet metal applications and comfortably processes mild steel up to roughly 12mm–15mm. A 6kW CNC laser cutter often represents the best balance between versatility and affordability. It can handle diverse production schedules without carrying the premium cost associated with ultra-high-power systems.

8kW–10kW: Throughput Accelerator

Stepping into the 8kW–10kW category dramatically changes productivity. Shops cutting large volumes of material between 3mm and 15mm often see substantial cycle-time reductions. Machines in this category also expand thick-plate capabilities, making them attractive for growing fabrication companies that need more production flexibility.

12kW–15kW: Production-Class Performance

At 12kW–15kW, laser cutting machine performance enters a different category altogether. Many applications that previously required plasma or legacy CO2 laser machine systems can now be completed using high-powered fiber technology. Materials in the 20mm–25mm mild steel range become routine production work, opening new revenue opportunities for manufacturers serving heavy industrial markets.

15kW–30kW: Maximum Capability

The 15kW–20kW segment pushes fiber laser cutting into territory once dominated by plasma and oxyfuel cutting equipment. Thick plate, challenging materials, and high-volume production become practical and profitable.

Mazak’s Optiplex HP platform supports power levels up to 3020kW and incorporates Variable Beam technology that optimizes beam characteristics for different material types and thicknesses.

One important consideration is diminishing returns. Moving from 4kW to 8 W can nearly double cutting performance on certain thin materials. However, gains become less dramatic above 10kW unless a shop regularly processes thicker materials or requires maximum throughput.

The Material x Thickness x Power Matrix

Selecting a laser cutting machine isn’t simply about choosing the highest available power. Material type and thickness must be evaluated together. For industrial sheet-metal fiber lasers, common power requirements run roughly 1kW–6 kW for general sheet metal, scaling upward with thickness and harder materials.

Mild steel serves as the baseline for most laser cutting discussions. It generally requires less power than many alternative materials and delivers predictable results across a wide range of thicknesses. Stainless steel presents a different challenge. While it remains highly compatible with fiber laser cutting machine technology, it often requires additional power and nitrogen assist gas to maintain edge quality. Shops specializing in stainless fabrication frequently benefit from moving into higher power tiers sooner than mild steel-focused operations.

Aluminum introduces another variable. Thin aluminum processes efficiently on many laser machines, but thicker sections require substantially more energy because aluminum rapidly dissipates heat. As thickness increases, power requirements rise faster than many buyers initially expect.

Reflective metals such as copper and brass historically posed challenges for older laser systems. Modern fiber laser cutter technology has largely solved these issues, but production-level copper processing typically starts around 6kW and often benefits from 15kW or greater power levels.

This is where application engineering becomes critical. Capital Machine’s approach emphasizes matching actual customer part mixes to machine capability rather than simply recommending the largest available system. Our Mazak portfolio covers the full sweep from sub-4kW through 20kW. Whether a customer needs an entry-level solution or a high-powered Mazak OPTIPLEX NEO, the recommendation is based on production requirements, not maximum specifications.

Beyond Power: Bed Size, Cutting Head, and Beam Shaping

Once power has been determined, secondary machine specifications come into focus.

Bed Size Considerations

Bed size should accommodate both current and future production requirements. For many North American fabrication shops, a 5-foot x 10-foot work envelope represents the ideal balance of flexibility and floor space efficiency. Production-oriented operations often move to 6-foot x 12-foot or larger formats to support larger sheet sizes and maximize throughput.

The Importance of the Laser Head

The laser head is one of the most critical components of any CNC laser system. It houses the focusing optics, nozzle, sensors, and other process-control technologies that directly influence cut quality. Modern laser heads automatically adjust focal positions based on material thickness and type. This automation reduces setup time and improves consistency across diverse production schedules.

Beam Shaping Technology

Advanced beam shaping represents one of the most significant recent innovations in industrial laser cutting.

Mazak’s OPTIPLEX NEO incorporates Variable Beam and Beam Diameter Control technology, allowing the machine to modify beam characteristics based on the cutting application. This improves performance across thin and thick materials while helping close the historical edge-quality gap between fiber laser and CO2 laser systems.

Flying Optics Systems

The Mazak OPTIPLEX FIBER III utilizes a flying-optics architecture in which the sheet remains stationary while the cutting assembly moves. This reduces moving mass, improves acceleration, and enhances productivity on complex nested parts.

Despite the importance of these features, they remain secondary to choosing the correct power tier.
An improperly sized power source will limit performance regardless of bed size or optics technology.

Software, Automation, and the Cost of Underpowered Controls

The physical laser cutter often receives the most attention during equipment evaluations, but software and controls frequently determine long-term success. CAM and nesting software directly influence material utilization. Even a modest 5% improvement in yield can generate substantial savings for shops running high-volume production.

Material handling automation creates another layer of productivity. Automated load/unload towers, shuttle tables, and storage systems allow a CNC laser cutter to operate unattended for extended periods, maximizing machine uptime while reducing labor requirements.

Control Systems Should Support

  • Offline programming
  • Automatic parameter optimization
  • Remote diagnostics
  • Process monitoring
  • Integrated production management

Modern Mazak laser machines include advanced control capabilities designed to simplify operation while maximizing productivity. One of the most common reasons a capable laser engraver, laser cutter, or industrial laser cutting machine becomes underutilized is poor software implementation.

Capital Machine’s engineers address this challenge early in the purchasing process by evaluating software and automation requirements alongside machine specifications rather than treating them as optional add-ons.

For customers evaluating long-term service and support requirements, Capital Machine also provides ongoing application assistance and technical resources through its service organization. We offer six core service categories: break-fix repairs, condition-based maintenance and preventative maintenance, installation supervision, operator training and retraining, application support and retrofits. Visit our service page.

Total Cost of Ownership: Power Draw, Assist Gas, and Maintenance

A complete laser cutter selection process must include total cost of ownership analysis. Fiber technology
has fundamentally changed operating economics compared to traditional CO2 laser machine systems.
Fiber systems typically consume significantly less energy while delivering dramatically higher cutting speeds.

Fiber operating costs run roughly $4/hour vs around $20/hour for CO2. The gap widens as power and utilization climb.

Assist gas is often one of the largest ongoing operating expenses. Nitrogen dominates stainless steel and aluminum applications because it produces clean, oxide-free edges. Oxygen remains common for mild
steel and offers lower operating costs, although edge characteristics differ. At high utilization rates, bulk
gas contracts frequently deliver substantial savings compared to cylinder-based supply models. Fiber sources are commonly rated for a minimum of 100,000 operating hours, versus roughly 25,000 hours for CO2. A major maintenance differential over a 10-year horizon.

Maintenance requirements also favor fiber laser cutting machine technology. Modern fiber sources are commonly rated for extremely long operational lifespans, reducing maintenance costs and minimizing downtime compared to legacy resonator-based systems. Higher-power machines naturally consume more electricity. However, they often complete jobs so much faster that energy consumption per finished part can actually decrease. This is one reason many manufacturers discover that moving to a higher-powered fiber laser cutter improves overall economics despite increased connected load requirements.

Capital Machine typically incorporates power consumption, gas costs, preventive maintenance planning, and productivity projections into the financial evaluation process to ensure customers understand the full ROI picture. We offer no-obligation consultations to discuss your shop’s specific requirements, production goals, and budget. Whether you are adding capacity, replacing aging equipment, or entering a new market, we can help. Contact us today.

Reflective Metals, Special Materials, and Edge-Case Selection

Certain applications require special attention during the laser cutter selection process. Copper and brass strongly favor fiber laser technology. Unlike many legacy CO2 laser systems, modern fiber platforms process reflective metals safely and efficiently. Production environments often benefit from 6kW or greater power levels, with 10kW+ systems preferred for thicker stock.

Titanium presents different challenges. While it cuts effectively using fiber laser cutting, maintaining assist-gas purity becomes critical. Many aerospace and medical manufacturers also implement additional inspection procedures to verify edge integrity. Modern Mazak systems incorporate back-reflection protection technology that helps safeguard optics and laser sources when processing highly reflective materials.

Despite the advantages of fiber technology, CO2 laser systems still maintain relevance for certain non-metal applications. Materials such as wood, acrylic, leather, and other organics often process more effectively on
CO2 laser machine platforms because fiber wavelengths do not couple efficiently with these materials.

Capital Machine’s brand-agnostic approach means a shop focused on copper fabrication may receive a very different recommendation than one specializing in stainless steel, even if both produce similar annual volumes.

From Spec to Floor: How to Validate a Laser Before You Sign

The final step in purchasing a laser cutting machine is validation. Rather than relying exclusively on specification sheets, shops should test real production parts. Bring your most challenging components, including thick plate, stainless steel, aluminum, copper, or brass parts, to one of our six technology centers.

Our centers are under power, so you can test out our systems under real world conditions. Our technology centers are located in Tampa, Florida; Atlanta, Georgia; Dallas, Texas; Indianapolis, Indiana; and Harrisburg, Pennsylvania.

When evaluating machines, shops should request cut-time benchmarks for actual parts at multiple power levels. Generic speed charts rarely tell the complete story. Beyond performance metrics, buyers should evaluate service response times, parts availability, operator training programs, installation support, and application engineering resources.

Capital Machine also has 43-factory-trained field service and preventative maintenance engineers and a
53-member service department. We provide the largest dedicated service network in the United States, backed by more than 40 years of equipment expertise. We are a dealer, service provider, and value-added distributor that not only has the top-of-the-line machines for sale, but we also provide comprehensive services that keep equipment working. Contact us today.


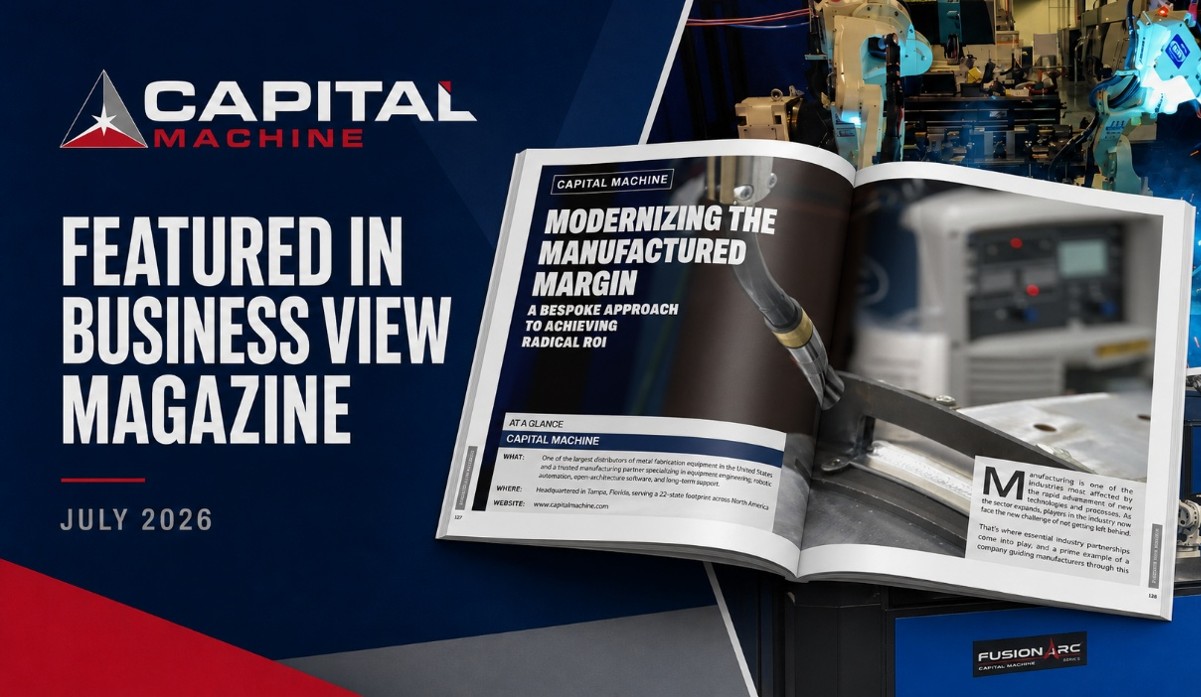
Capital Machine is proud to be featured in the July 2026 issue of Business View Magazine, highlighting our approach to helping manufacturers improve productivity, overcome labor challenges, implement automation, and make smarter investments in manufacturing technology.

The feature, “Modernizing the Manufactured Margin: A Bespoke Approach to Achieving Radical ROI,” takes an inside look at how Capital Machine has evolved beyond equipment distribution to serve as a long-term manufacturing partner for companies across a wide range of industries.

Building Solutions Around the Application

At Capital Machine, finding the right solution starts with understanding the customer’s operation. Rather than beginning with a specific machine or technology, our team works to identify where production is being limited, whether by labor constraints, throughput, quality, downtime, or other challenges.

That consultative approach allows us to recommend technology based on the customer’s actual application and long-term goals.

The Business View feature also explores how Capital Machine uses ROI calculations, cycle-time analysis, equipment demonstrations, automation, and open-architecture software to help manufacturers make informed investments. This includes finding opportunities to integrate new technology with existing equipment rather than assuming modernization requires replacing everything already on the shop floor.

Preparing Manufacturers for What Comes Next

As manufacturing continues to evolve, automation, advanced software, and workforce development will play an increasingly important role in remaining competitive.

The feature highlights Capital Machine’s belief that automation is not simply about replacing manual work. It is about helping manufacturers use their people more effectively, develop new skills, improve productivity, and build stronger operations for the future.

We appreciate Business View Magazine for the opportunity to share more about Capital Machine, our team, and the approach we bring to manufacturers across our 22-state footprint.

Read the full Capital Machine feature beginning on page 127 of the July 2026 issue of Business View Magazine:

Read the Full Feature

Staff-Doug-Peoples-square-f102801acfb3c0804c97278e47599dbb-

Doug Peoples has more than 20 years of territory experience and works closely with customers to identify the right fabrication solutions. Doug focuses on long-term customer relationships, guiding manufacturers through phased capability expansion and strategic capital planning to support sustained growth.

Where It Started

Nearly 20 years ago, this customer purchased their first CNC press brake from Capital Machine — an Accurpress 7 Series 250 with an ETS 3000 control.

At the time, it was simply the right machine for what they needed. But that first purchase became the beginning of a relationship that would continue as their operation grew and changed.

Growing With Their Needs

Over the years, their needs became more complex. They added larger Accurpress Excels with advanced 6-axis backgauges, plasma cutting systems, multiple flat lasers, OMAX waterjet technology, robotic welding and CNC sawing systems.

Each new piece of equipment came at a different point in the company’s growth. Sometimes they needed more capacity. Other times, they were looking to bring a new process in-house or improve the way a part was being made.

As those needs changed, so did the conversations.

Rather than looking at each machine as a separate purchase, the focus became understanding where the customer was headed and what equipment made sense for that next step.

The Next Step

Most recently, that next step was large-format tube laser cutting.

The new system gives the customer the ability to take parts from 3D models directly into production while bringing more of the manufacturing process under their own roof. It reduces their dependence on outside suppliers and gives them more control over how and when parts are produced.

What stands out about this latest project is that the customer came to Capital Machine with the need already in mind.

After nearly two decades of working together, they knew who to call.

A Relationship Built Over Time

That kind of relationship doesn’t come from one machine sale. It develops over years of conversations, service, changing production needs and finding the right solution when the next challenge comes along.

Looking back, the customer’s operation today looks very different from where it started nearly 20 years ago. The equipment has changed, their capabilities have expanded and new technologies have been added along the way.

But the relationship has continued through each stage.

Looking Ahead

For manufacturers, growth rarely follows a perfectly planned path. One investment leads to another as new customers, new parts and new opportunities come along.

Having a partner who understands where you’ve been can make those next decisions a little easier.

For this customer, what started with one press brake nearly 20 years ago has grown into a much broader manufacturing operation — and a partnership that has grown right along with it.

A Partnership Framework for Growth

Before making your next capital equipment decision, consider:

  1. Does this investment expand capability or just capacity?
  2. How does it integrate with existing systems?
  3. Will it reduce external dependencies?
  4. Does it align with long-term manufacturing strategy?
  5. Are you working with a partner who understands your evolution?

These questions can help make sure the next investment supports where your operation is going, not just what it needs today.