Alec Cuellar is a Sales Engineer with Capital Machine, specializing in advanced fabrication solutions that empower manufacturers to scale with precision and efficiency. Alec partners with customers to help them integrate cutting-edge technologies that accelerate innovation in industries ranging from energy to aerospace


For a growing manufacturer, adding equipment can be about much more than increasing production capacity.

Sometimes, it’s about gaining control over a process that has been outside the building.

That was the opportunity for Mill Scale Metalworks, a Lockhart, Texas manufacturer known for premium BBQ pits, smokers, and live-fire cooking equipment.

As the company continues to grow, Mill Scale is working toward becoming a more self-sustaining manufacturer by bringing key fabrication processes in-house.

The Challenge: Dependence on Outside Forming

Before this investment, Mill Scale subcontracted much of its forming work to another Capital Machine Technologies customer in the Austin area.

That arrangement gave Mill Scale access to the forming capacity it needed, but it also meant working around an outside supplier’s schedule and pricing.

As production grows, that can make it harder to respond quickly to changes in demand, control lead times, and manage the cost of each product.

The Solution: An Accurpress Press Brake

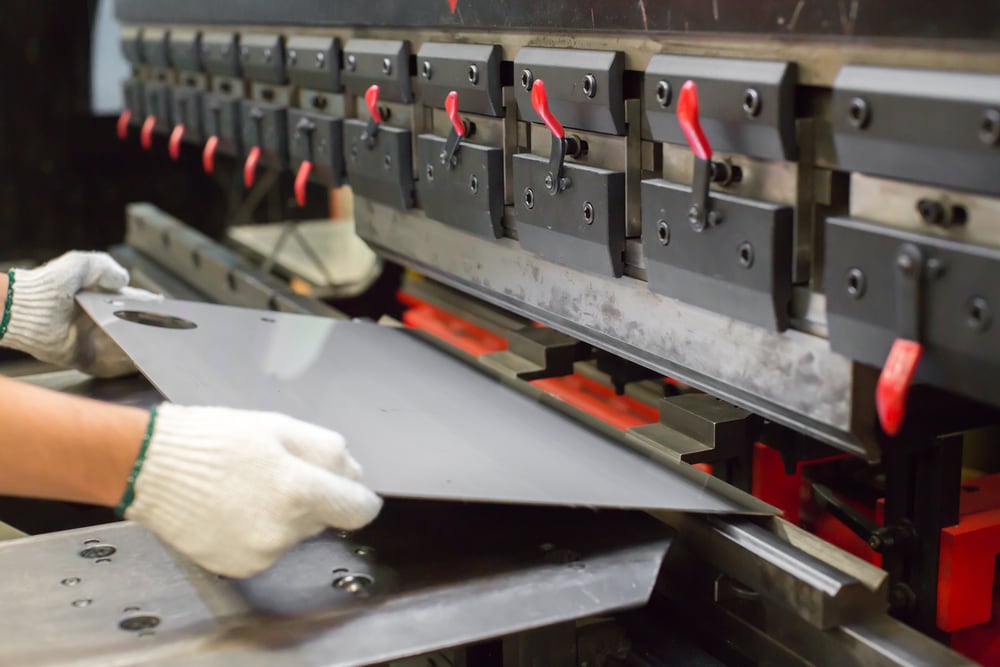
To bring forming under its own roof, Mill Scale invested in an Accurpress press brake.

The new capability gives the team direct control over a critical part of its manufacturing process.

Instead of sending forming work outside, Mill Scale can produce parts when they are needed and adjust production more directly around its own schedule.

The Result: More Control Over Production

With forming now in-house, Mill Scale can:

  • Reduce dependence on subcontractors
  • Improve control over production scheduling
  • Respond faster to production changes
  • Shorten lead times
  • Better control cost per product
  • Add capacity to support future growth

The value of the investment goes beyond the press brake itself. Bringing forming in-house gives Mill Scale greater control over how and when an important part of its products gets made.

Building Toward Greater Vertical Integration

The Accurpress is an important first step in Mill Scale’s broader manufacturing strategy.

As the company continues to grow, Capital Machine Technologies will also work with the team to evaluate laser cutting solutions.

The goal is to bring even more of the fabrication process under one roof.

That approach can help Mill Scale reduce outside manufacturing costs, improve throughput, and build a more scalable operation that can support continued growth.

A Practical Question for Growing Manufacturers

For manufacturers that rely on subcontractors for key fabrication processes, it can be worth looking at the bigger picture.

Consider:

  1. Which processes create the most dependence on outside suppliers?
  2. How much do subcontracting costs affect your products?
  3. How much control could you gain by bringing that work in-house?
  4. Would additional equipment help shorten lead times?
  5. Could bringing one process in-house create a path toward greater vertical integration?

The right equipment investment can do more than increase capacity.

It can give a manufacturer greater control over its production and create a foundation for the next stage of growth.

For Mill Scale, that journey starts with bringing forming in-house with an Accurpress press brake.

Brent Anderson is Vice President of Sales at Capital Machine and a trusted advisor to manufacturers adopting robotic welding and automation. With decades of experience helping customers identify high-impact applications and validate ROI before investing, Brent helps fabrication leaders automate with confidence.

Continue reading “When to Choose a Small Press Brake for Your Shop”

Clint Harrison is a robotic welding and advanced automation specialist at Capital Machine Technologies. With extensive experience integrating robotic cells with intelligent fixturing and part-recognition systems, Clint helps manufacturers design scalable automation platforms that reduce manual intervention and support sustained production growth.


For many fabrication shops, press brake productivity is about more than how quickly a machine can bend a part.

Setup time, first-part accuracy, and the amount of rework required before production begins can have just as much impact on overall efficiency.

One customer came to us with problems in all three areas.

Long Setups and Too Many Reruns

The customer was spending 30, 45, and sometimes nearly 60 minutes setting up their press brake just to get the first part ready.

Accuracy created another bottleneck.

Operators had to send their first parts to quality for measurement. When parts failed, programmers had to adjust the programs and rerun them. The parts went back to quality, and the process repeated until they had an acceptable part.

The result was lost production time, added labor, and unnecessary scrap.

A More Precise Press Brake Setup

After reviewing the customer’s process, I recommended a Safan E-Brake with Wila hydraulic clamping and Smart Tool Locator.

The combination addressed both sides of the problem: setup efficiency and part accuracy.

The E-Brake’s all-electric design provided the accuracy the customer needed, while the tooling and setup configuration helped streamline the process.

The Result: Setup in Minutes

The customer reduced press brake setup times from as much as an hour to a couple of minutes.

Improved accuracy also helped the team achieve first-part-right production, reducing the need for repeated measurements, program adjustments, and reruns.

That meant:

  • Less time spent setting up
  • Fewer parts sent back for adjustment
  • Less rework
  • Reduced scrap
  • More time available for production

The improvement wasn’t simply about making the press brake faster. It was about removing the delays and corrections that were happening around the machine.

A Practical Question for Your Press Brake Operation

If your team is spending significant time getting the first part right, look beyond the machine’s bending speed.

Consider:

  1. How long does setup take today?
  2. How many first parts need to go through quality?
  3. How often do programs need to be adjusted and rerun?
  4. How much production time is lost before the job is truly underway?
  5. Could improved tooling and machine accuracy reduce those steps?

A press brake should help your team start producing good parts quickly, not spend the first hour of every job getting there.

This customer saw the difference firsthand. They now have five Safan press brakes in their operation.

The right combination of machine, tooling, and setup strategy can turn a recurring production bottleneck into a much more efficient process.

Rick Szepski works with fabricators and manufacturers across Indiana on cutting, plate rolling, forming, and structural processing solutions at Capital Machine. Rick helps shops identify the bottleneck limiting their next stage of growth and match it with equipment that fits their parts, their people, and their floor space.


A trailer manufacturer. A container services company. A structural fabricator. Three shops in three different industries, each up against a different wall — and together they show that while no two shops hit the same bottleneck, the way through it starts in the same place every time.

Not with a machine. With the bottleneck.

The Trailer Manufacturer That Brought Rolling In-House

A southern Indiana trailer manufacturer was outsourcing a significant amount of rolling work, and the volume had reached the point where bringing it in-house made sense. Here’s the part I like: the shop they had been outsourcing to is a Capital Machine customer running the machinery we represent — and gave that equipment its highest recommendation. The endorsement came from the very shop that stood to lose the work.

The technical challenge was a very particular roll profile shape that had to be achieved. Rather than asking the customer to take that on faith, DAVI and Capital Machine consulted with them directly on the best way to produce that profile before any equipment was purchased.

The customer invested in a Messer 8’ x 20’ EdgeMax cutting machine and a DAVI CNC plate roll. Just as important to them as the machines themselves: they wanted technology that is well supported and has a strong presence in the industry, so they wouldn’t be on their own after installation.

Today they see us as a trusted partner, and we’re already discussing the next round of fabrication improvements — in forming and robotic welding.

The Forming Department Where Every Operator Runs the Same Program

A container services company has been a customer for years, adding press brakes, plasma tables, and robotic welding systems as it grew. Its next challenge was different: the forming department needed more throughput, but its operators covered a wide range of skill levels. Output depended heavily on who was standing at the machine.

The solution had two parts. The first was an Accurpress Accell U press brake, with additional stroke, more open height, and faster forming speeds. The second — and in some ways the more important one — was Radan offline nesting and bending software.

With Radan, machine programming happens in the office instead of at the control. Programs arrive at the brake ready to run, so an operator at any skill level can set up and run the machine efficiently. The press brake got faster, but the whole department got more consistent — and that’s where the throughput came from.

The Structural Fabricator That Ended Mag Drilling

A long-term customer in the structural steel business set a clear goal: bring structural processing in-house and eliminate the manual mag drilling and structural layout that was consuming skilled labor on every job.

They initially looked at large drill line systems, but their space constraints made those a difficult fit. The answer was an Ocean Avenger Plus CNC drill line paired with an Ocean Liberator CNC coping machine — equipment that fit the floor they actually have.

We also planned the equipment layout around where the shop is headed, not just where it is: it leaves room to add a large structural bandsaw and blasting equipment later. What the customer valued most was the breadth — deep knowledge of the structural industry and a wide enough range of solutions to match the machine to the building, instead of the other way around.

One Approach

Three shops. A trailer manufacturer paying someone else to roll its plate. A forming department whose output depended on who was running the brake. A structural fabricator laying out and mag drilling steel by hand.

Different industries, different bottlenecks, and three completely different equipment answers — a plate roll, a press brake with offline programming, a drill line and coping machine. If we had started any of these conversations with a machine recommendation, we would have gotten at least two of them wrong.

The approach that worked in all three cases is the same one we bring to every shop: find the constraint that’s holding back the next stage of growth, then match it with equipment that fits the parts, the people, and the floor space — backed by support that’s still there long after installation.

The machine comes last. The bottleneck comes first.

Why the Right Press Brake Makes or Breaks Your Shop’s Profitability

Press brakes represent a significant capital investment for any organization. Costs typically range from $150,000 for mid-range hydraulic models to $500,000+ for high-end computer numerical control (CNC) and electric configurations depending on the length and tonnage. This makes the selection decision one of the highest-impact equipment choices a fabrication shop will face. How to choose a press brake, and the right one for your shop’s needs, can seem quite difficult.

Press brake selection directly affects your shop’s production efficiency and profitability by determining bending speed, setup times, and accuracy. This directly influences labor costs, material waste, and throughput. Below are some common buying mistakes to avoid.

Common Buying Mistakes to Avoid

  • Over-specifying tonnage: You end up paying for capacity you don’t need or use.
  • Under-specifying bend length: This can limit future job flexibility.
  • Ignoring the total cost of ownership: Maintenance, operator training, tooling, and press brake dies.

Capital Machine Technologies can make choosing the right press brake much easier. We can help by taking an advisory approach to press brake selection, evaluating each shop’s actual production mix, material types, and growth plans before recommending equipment. Our consultative process is built on 40+ years of working with job shops and mid-market manufacturers across 22 states.

This is why we have six technology centers under power for you to test out real-world applications. This allows you to make a much more informed decision. At each technology center we have our full lineup of press brake machines under power. Our technology centers are located in Tampa, Florida; Atlanta, Georgia; Norcross, Georgia; Dallas, Texas; Indianapolis, Indiana; and Harrisburg, Pennsylvania.

Hydraulic, Electric, or Hybrid: Which Press Brake Technology Fits Your Production

Finding the right press brake for your shop is critical. This is why Capital Machine offers hydraulic, electric, and hybrid press brakes for you to select from. Hydraulic press brakes, such as the Accurpress Advantage, Accell-E, Accell-U and Accell-HT, remain the workhorse of the industry. These models offer a high-quality build, an impressive number of features and options, and advanced controls.

Electric press brakes, like the SafanDarley E-Brake Series, deliver faster cycle times than conventional hydraulic machines, with lower energy consumption and reduced maintenance. SafanDarley is the innovator and patent holder for the first all-electric e-brake, first introduced in the mid-90s. The SafanDarley E-Brake ranges from 39 to 330 tons and has a complete range of options for specific applications. This makes electric press brakes ideal for shops running repetitive, precision-critical production.

Hybrid press brakes, such as the Accurpress Accell H, combine electric pump technology with hydraulic force delivery, offering energy efficiency, while maintaining the tonnage flexibility of hydraulic bending machines. This is a growing choice for shops balancing sustainability goals with heavy-duty bending machine requirements.

How to Calculate the Exact Tonnage Your Press Brake Needs

Tonnage requirements for your shop’s particular needs will depend on the material type, thickness, bend length, and die opening. The Rule of 8 is a good guide and the industry-standard starting point for calculating required force and selecting appropriate tooling for a press brake.

Different materials will require dramatically different tonnage for the same sheet metal thickness. Mild steel requires 60,000 PSI tensile strength and is the baseline at 1.0x. Stainless steel requires 90,000 PSI and roughly 1.5x the force. Aluminum requires roughly 0.5x the force. This makes material mix a critical input to the tonnage calculation and the bending force required.

Our advisory team can help shops avoid both over-specifying, or wasting capital on unused capacity, and under-specifying, or limiting future job capability, by analyzing actual production data and anticipated growth.

How Bend Length, Precision, and Tooling Shape Your Press Brake Decision

Bending length should be selected based on the longest part you regularly produce plus a margin for future work. Going too short locks you out of larger jobs, while excessive length adds cost without proportional benefit.

Precision requirements will vary by application. HVAC and general fabrication may tolerate +/- 1 to 2 degrees, while electrical enclosure work often demands +/- 0.5 degrees to maintain uniform door seams and gasket compression. The choice between air bending, bottom bending, and coining directly affects achievable bending accuracy.

Press brake tooling systems, such as American standard vs. European style, and manual vs. hydraulic clamping, affect both changeover speed and precision. Shops running high-mix production with multiple setups per day will see significant productivity gains from quick-change tooling systems.

Capital Machine can assist shops in finding the right press brake tooling to make your work easier. This will allow your shop to bend metal quicker and safer. Our six technology centers are a great place to test out your shop’s applications. Out centers are under power so you can test out our quick-change tooling systems and make test bends under real world conditions. Our technology centers are located in Tampa, Florida; Atlanta, Georgia; Norcross, Georgia; Dallas, Texas; Indianapolis, Indiana; and Harrisburg, Pennsylvania.

How CNC Controls, Back Gauges, and Automation Cut Your Setup Time

CNC press brakes with programmable back gauges and angle correction dramatically reduce setup time and operator dependency. This is critical for shops handling dozens of different parts per shift where manual adjustments on every bend would consume hours of productive capacity.

Advanced back gauge systems with multi-axis and programmable finger positioning, enable complex part geometries without manual repositioning. This is a feature that pays for itself quickly in shops producing parts with multiple bends at different depths and angles.

Robotic bending cells, such as the SafanDarley R-Brake, integrate the press brake with automated part handling, enabling lights-out or reduced-labor production. This is an increasingly viable option for mid-market manufacturers running higher-volume, repeatable parts.

Safety Features You Should Require Before Buying Any Press Brake

Modern press brakes should incorporate appropriate safeguarding, which may include light curtains, laser safety devices, two-hand controls, and emergency stop controls where applicable. OSHA’s general machine guarding requirements are established under OSHA 29 CFR 1910.212, with additional guidance for power press brakes provided in OSHA Directive STD-01-12-012.

Advanced safety systems, such as active knock-out avoidance systems, and laser beam safeguarding allow operators to work closer to the point of operation without sacrificing speed. This improves productivity, while maintaining compliance.

Space, Power, and Installation: What to Plan Before Your Press Brake Arrives

A press brake’s footprint varies significantly by tonnage and type. A 100-ton hydraulic machine measures approximately 11 feet–11.5 feet in length but requires 12 feet–14 feet including operator clearance zones. Tandem configurations for heavy plate work typically range 26 feet–39 feet making shop layout planning an essential pre-purchase step.

Electrical requirements range from single-phase 220V for smaller machines to three-phase 480V for high-tonnage hydraulic and electric models. Shops should verify transformer capacity before purchase to avoid costly electrical upgrades.

Capital Machine’s installation supervision covers the full process of installation with a pre-install site survey, machine calibration, first-run testing, and operator sign-off. Equipment placement is handled by a local rigger and utility connections by certified electricians, and all coordinated by our project management team.

How to Evaluate Your Press Brake Vendor: Beyond the Machine Itself

The press brake itself is only part of the investment and ongoing value depends on the vendor’s ability to deliver training, service, parts, and application support throughout the machine’s 15-year–25-year lifespan.

Key vendor evaluation criteria should include service response time and coverage area, availability of factory-trained technicians, training programs for operators, and whether the vendor offers condition-based maintenance to protect uptime, not just break-fix service after failures.

Capital Machine sets itself apart from other vendors with our post-purchase support. We are a dealer, service provider, and value-added distributor that not only has the top-of-the-line press brake machines for sale, but we also provide comprehensive services that keep equipment working.

Our 43 factory-trained field service engineers have parts-stocked vans and are ready to diagnose and service your equipment across our 22-state territory. Our engineers are backed by a 53-member service department ready to assist you. We offer six core service categories: break-fix repairs, condition-based maintenance and preventative maintenance, installation supervision, operator training and retraining, application support and retrofits. We provide the largest dedicated press brake service network in the United States, backed by more than 40 years of fabrication equipment expertise. Contact us today for more information.